At Prayosha Meera Spices, we are passionate about bringing the rich aroma, authentic taste, and natural goodness of premium spices to every kitchen. Every product is carefully sourced, expertly processed, and hygienically packed to preserve its freshness, purity, and exceptional quality. Backed by Prayosha Group, our infrastructure is built to turn raw spices into trusted, everyday kitchen essentials batch after batch, year after year. Our commitment is to deliver spices that inspire delicious meals and lasting trust.
Premium Quality
We carefully select the finest raw spices and maintain strict quality standards throughout processing and packaging, so every batch meets the same high benchmark.
Authentic Taste
Our expertly blended spices preserve traditional Indian flavors while delivering consistent taste in every pack, from the first pinch to the last.
Modern Manufacturing
Produced in a hygienic, state-of-the-art facility using advanced processing technology, our spices retain their freshness, colour, and aroma while meeting global food safety standards.
Customer First
Customer satisfaction is at the heart of everything we do. We strive to deliver products that families, chefs, and commercial kitchens can trust every day.
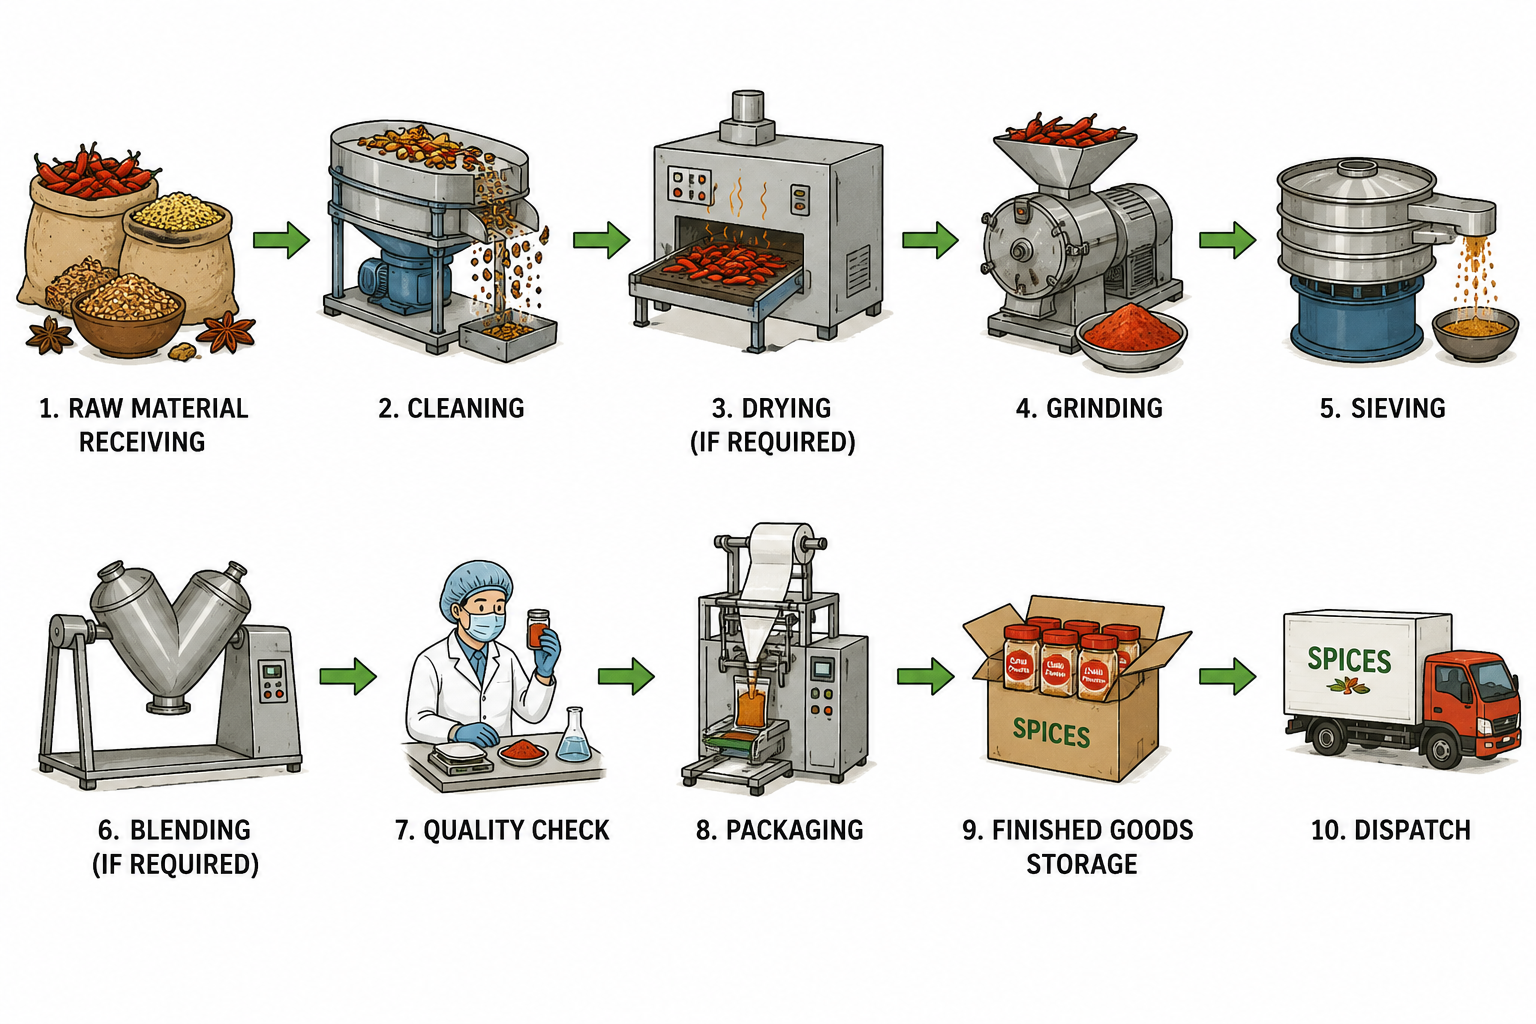
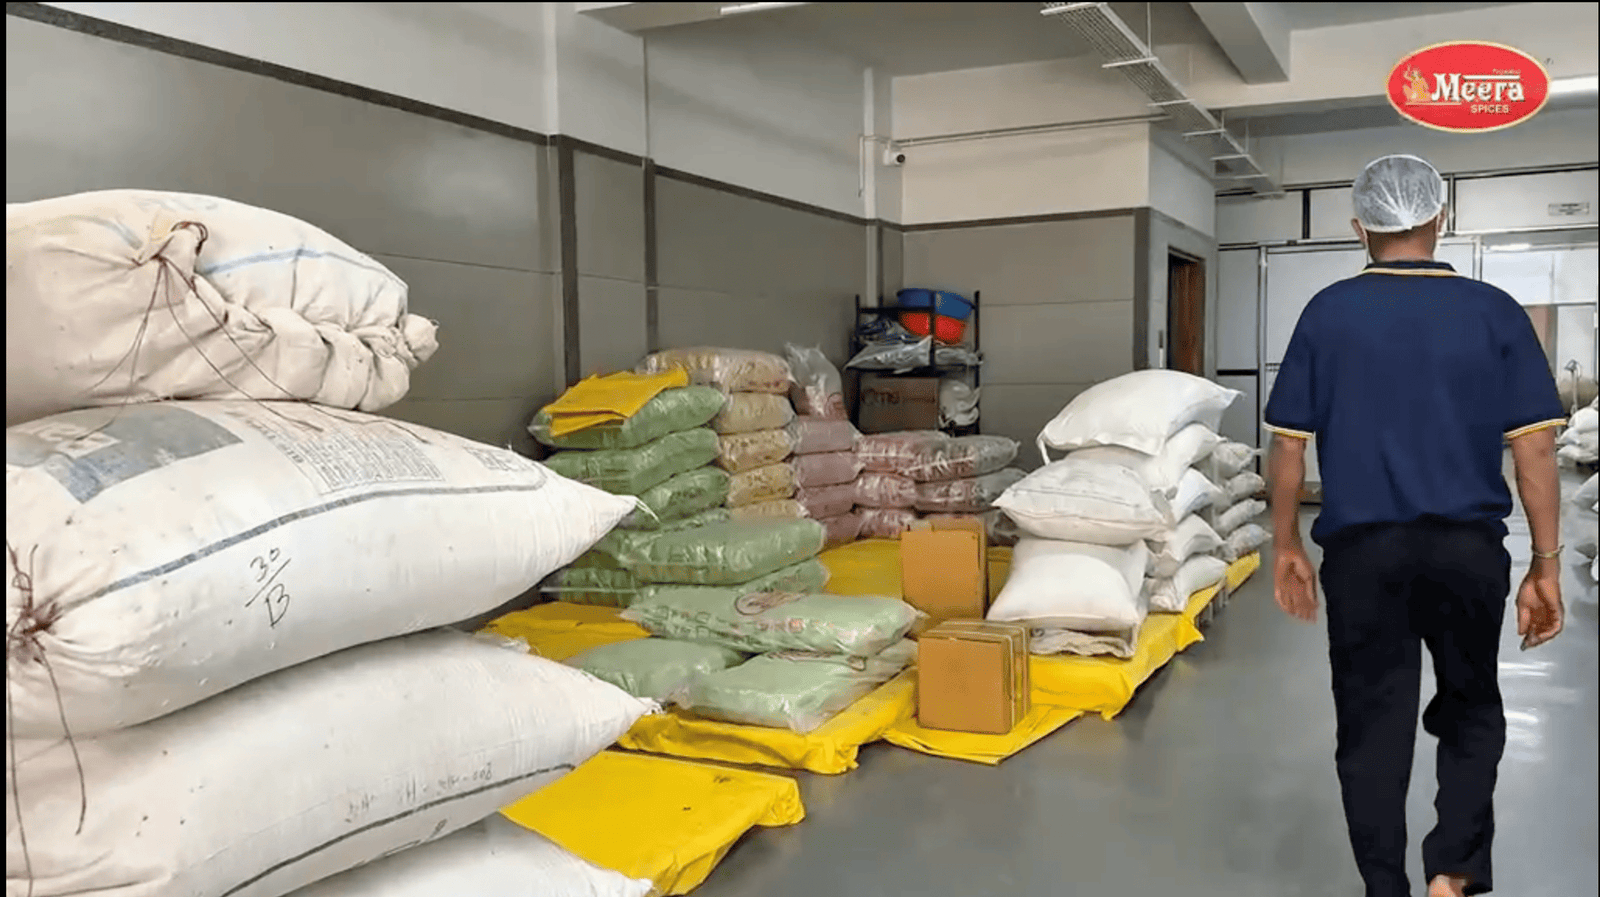
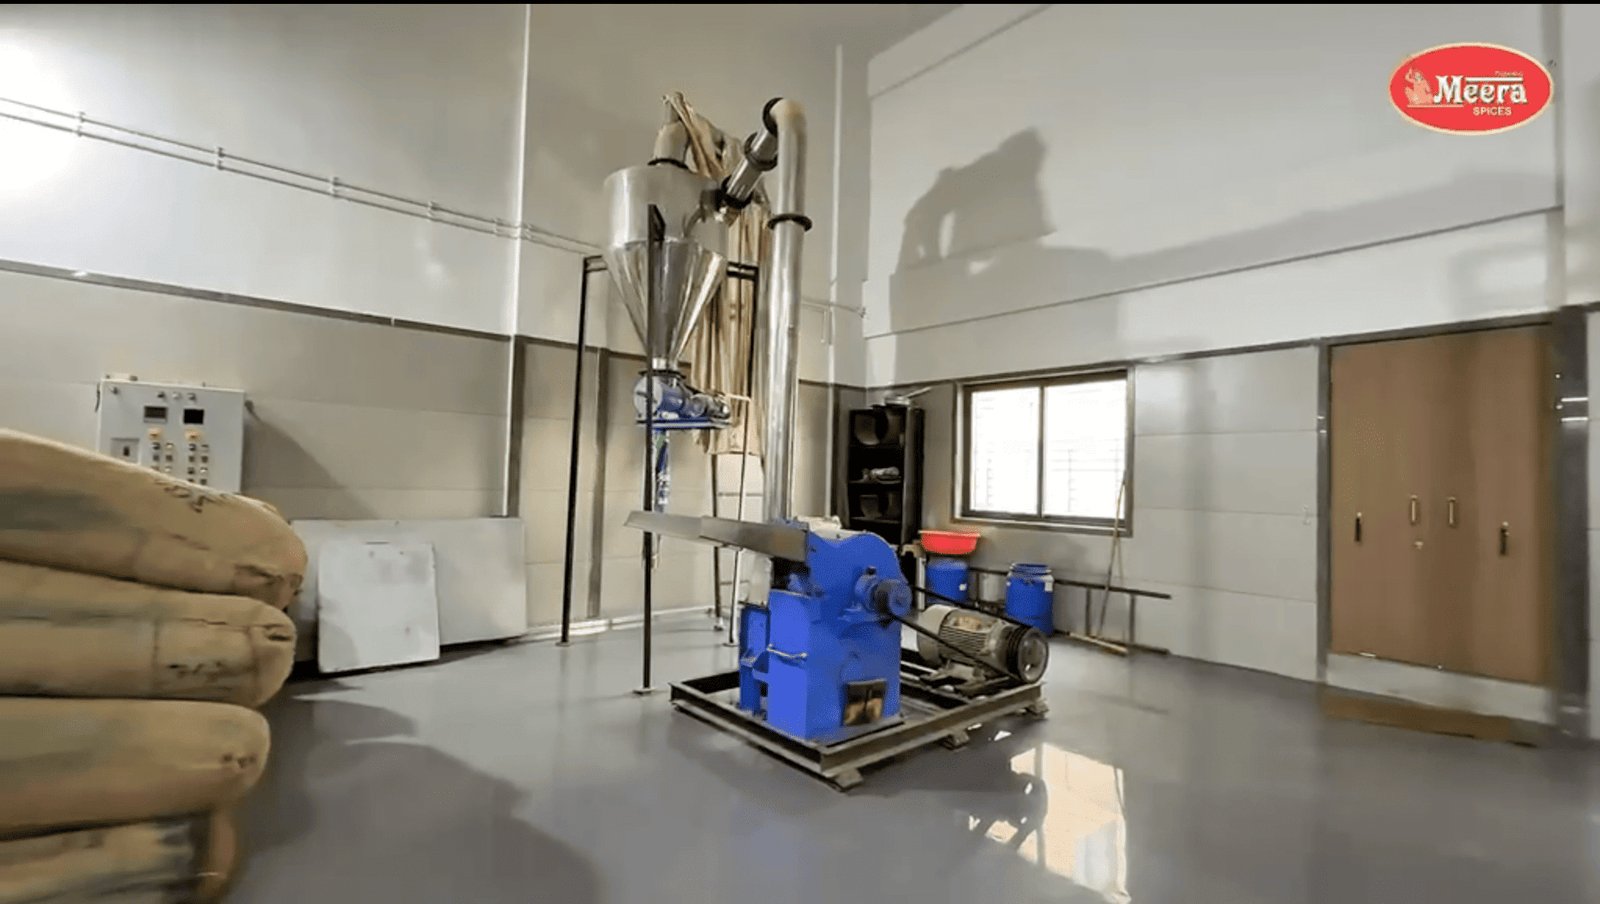
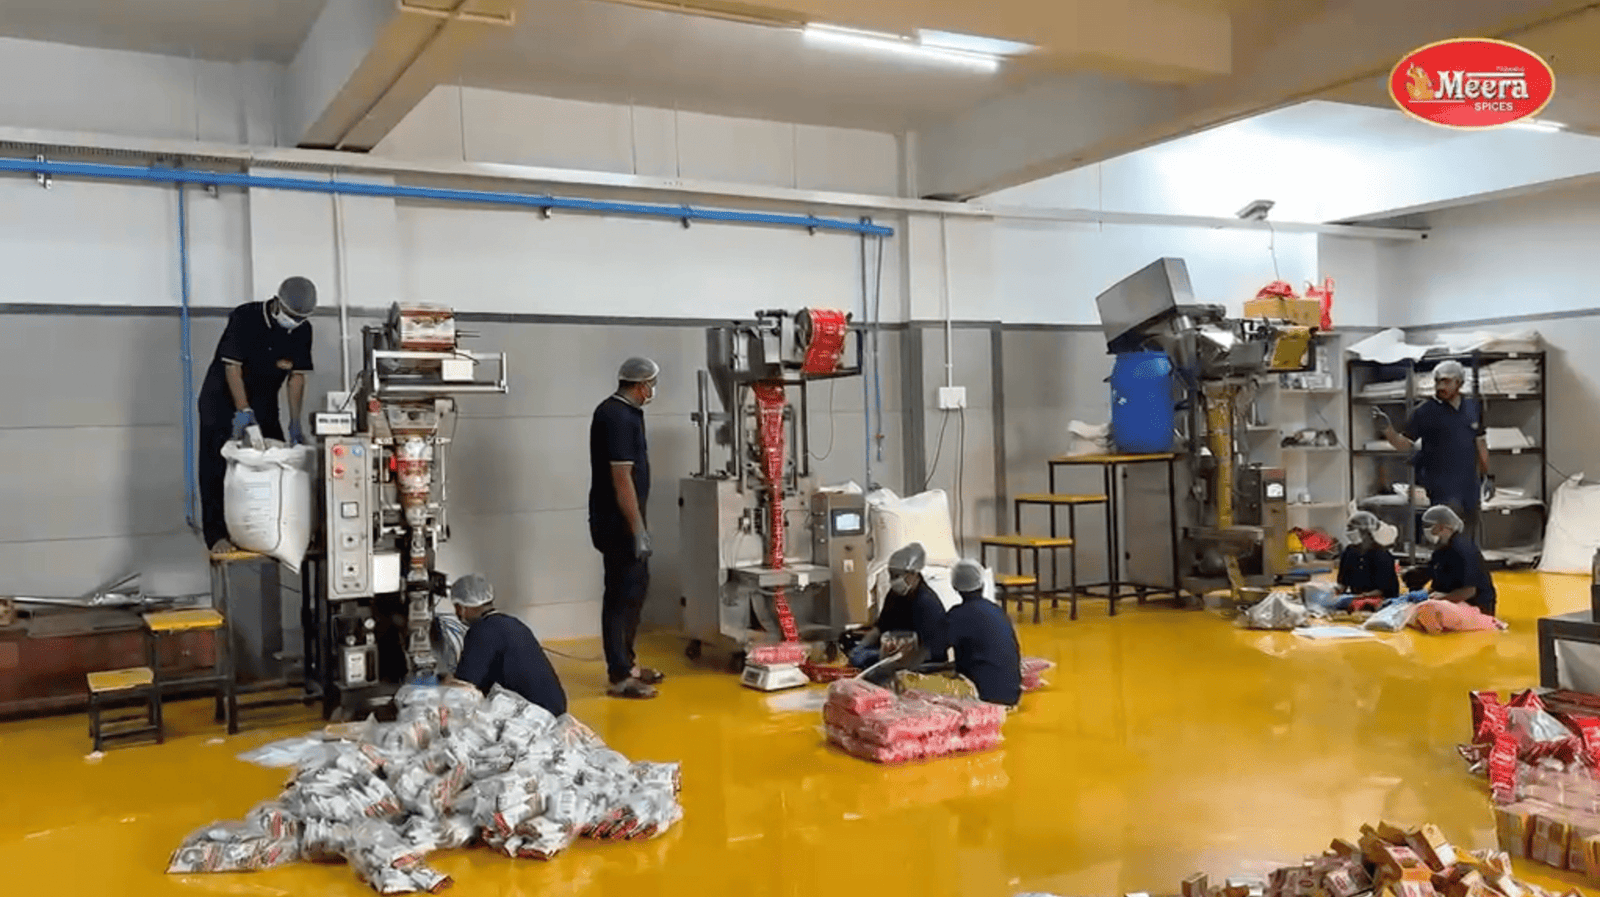
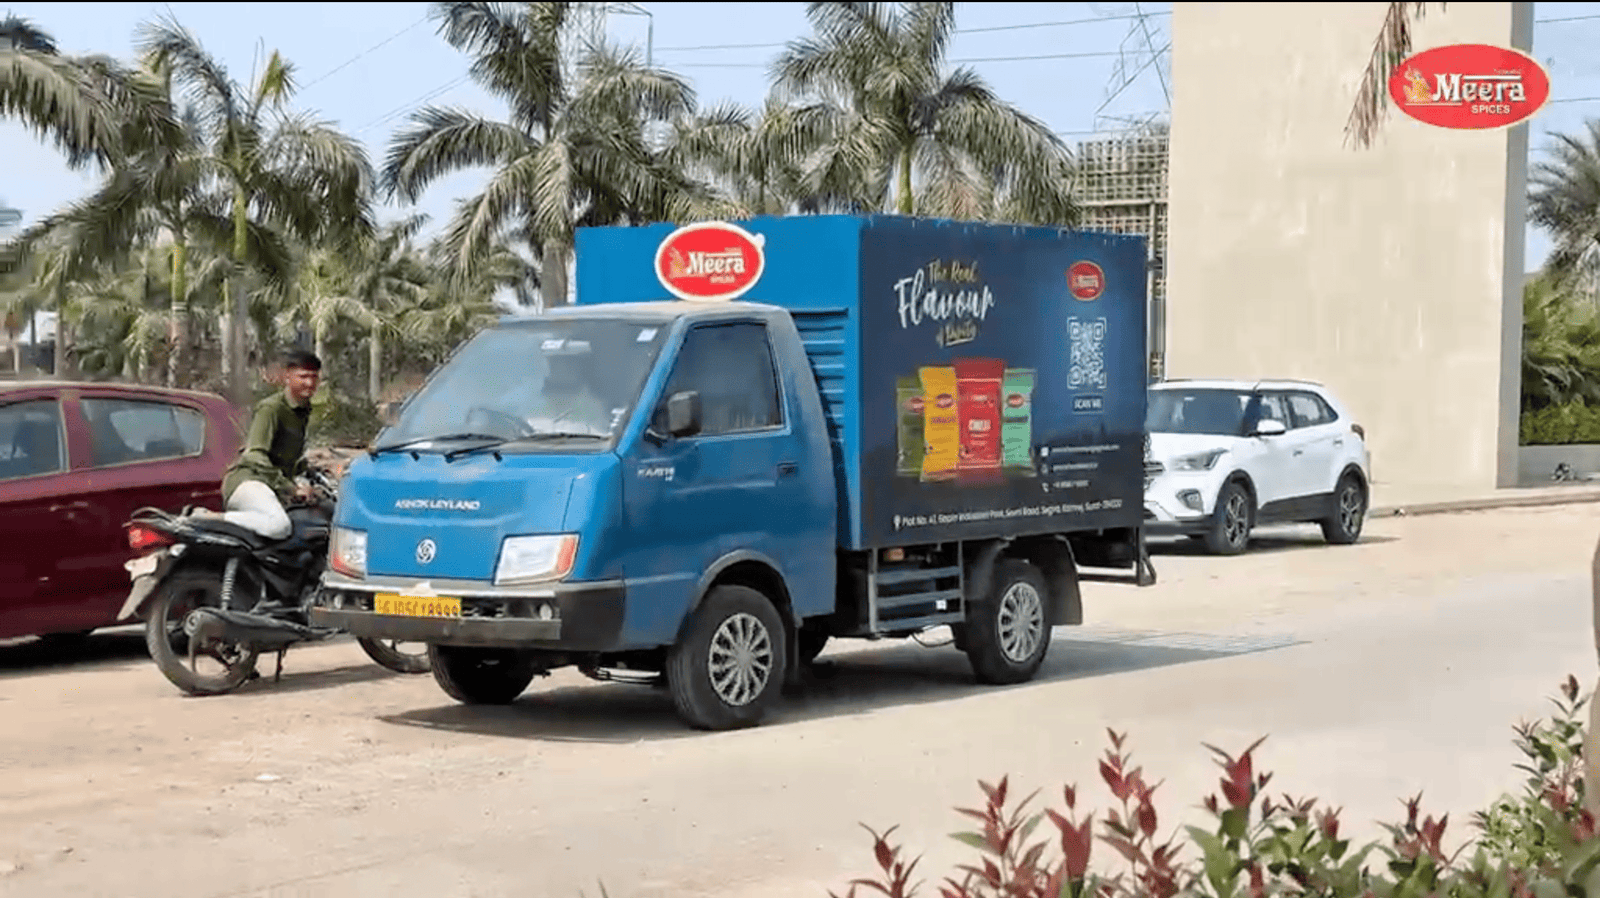
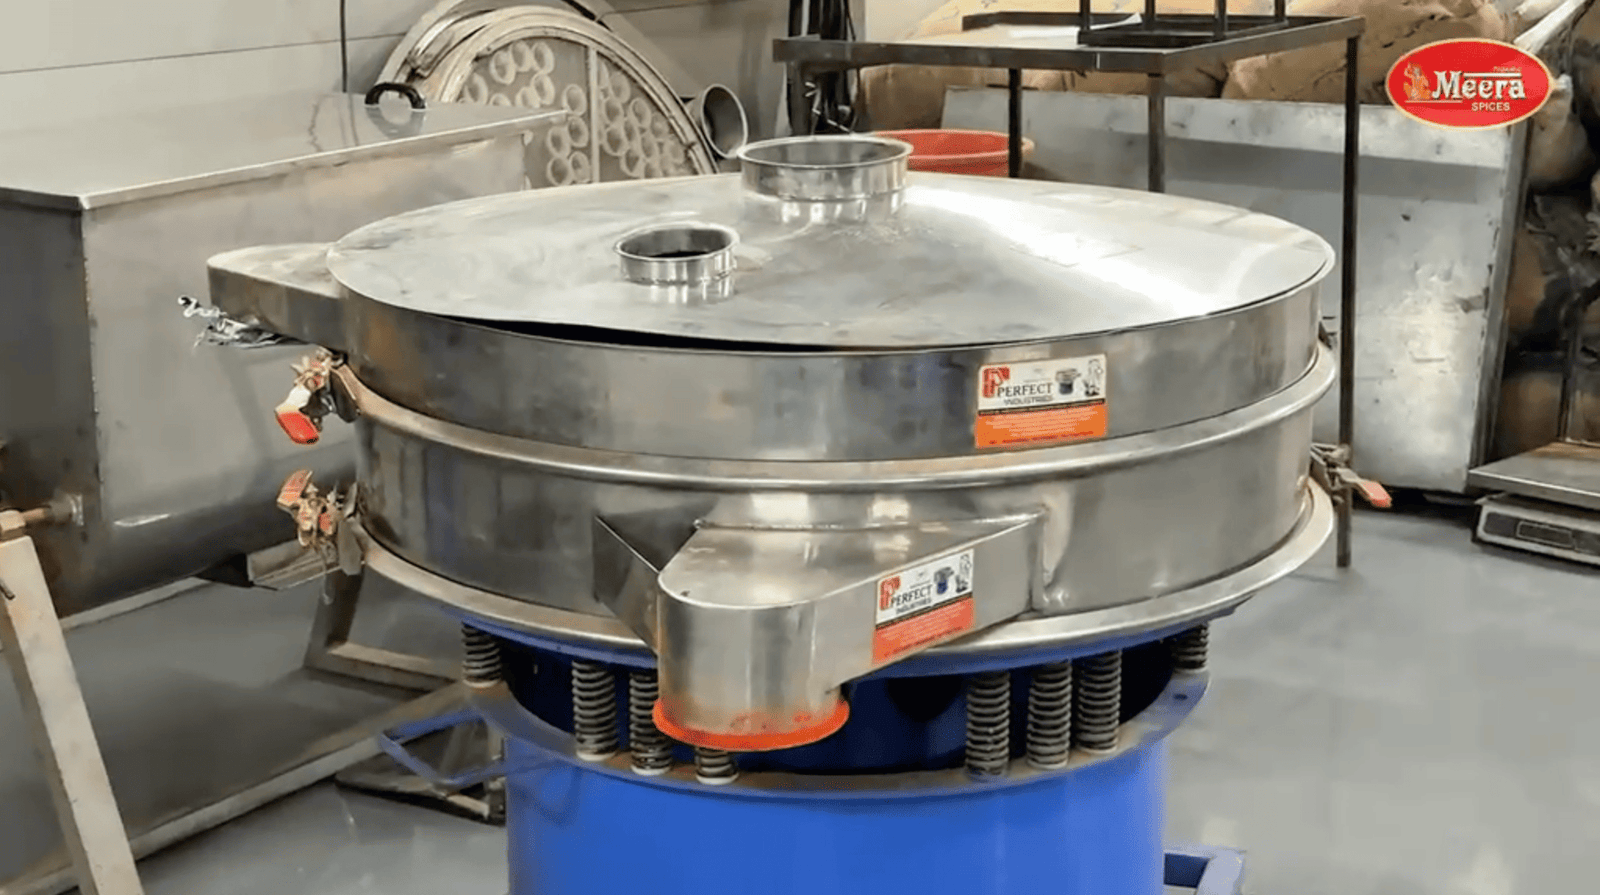
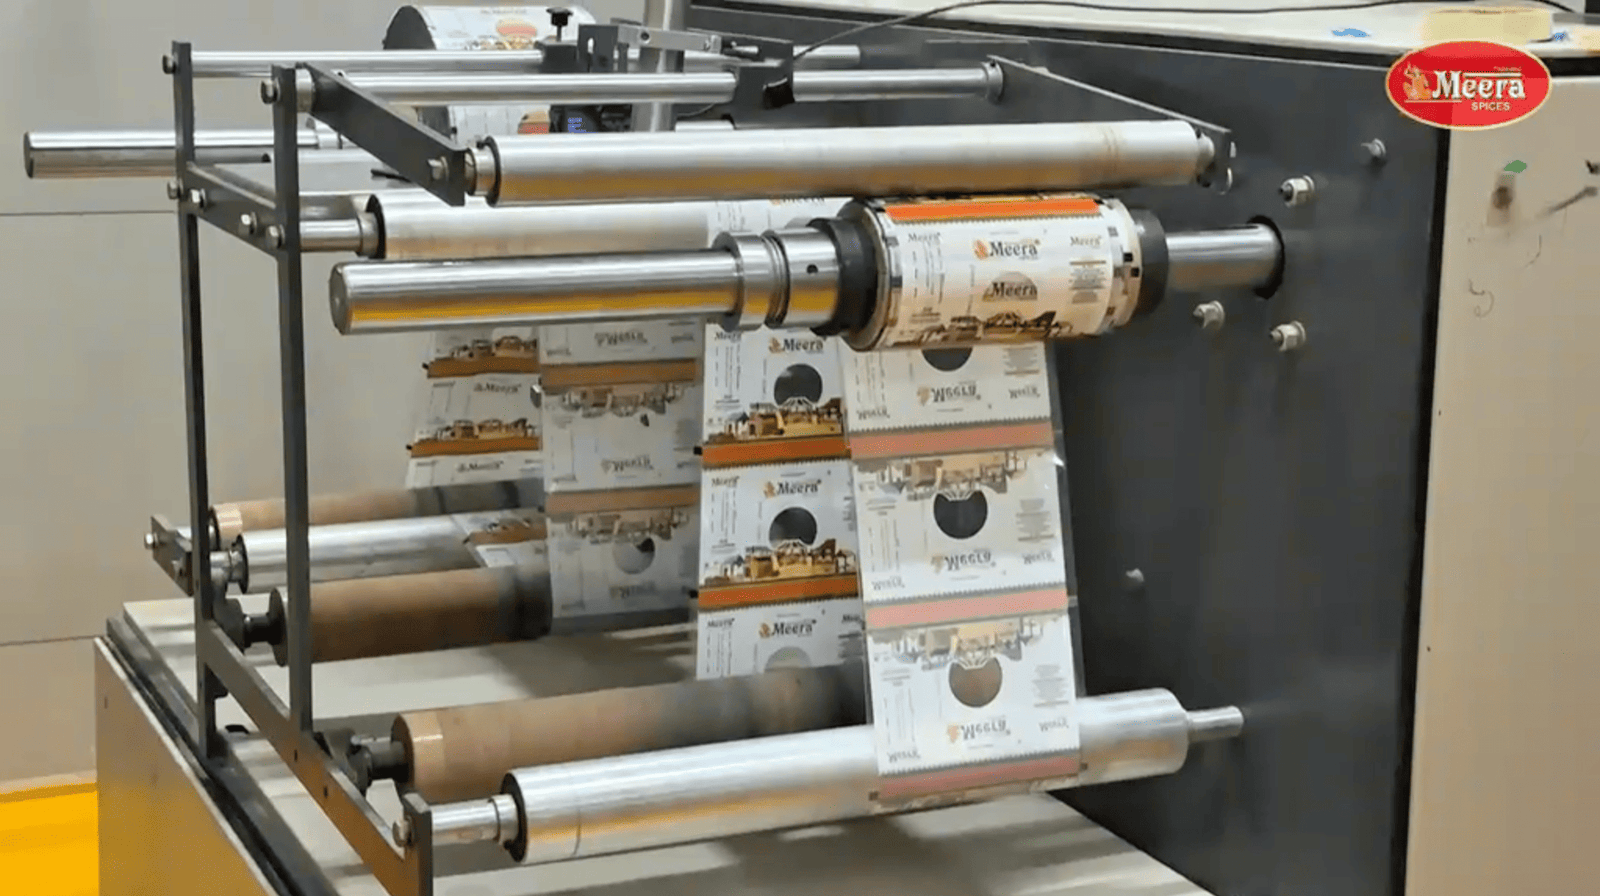
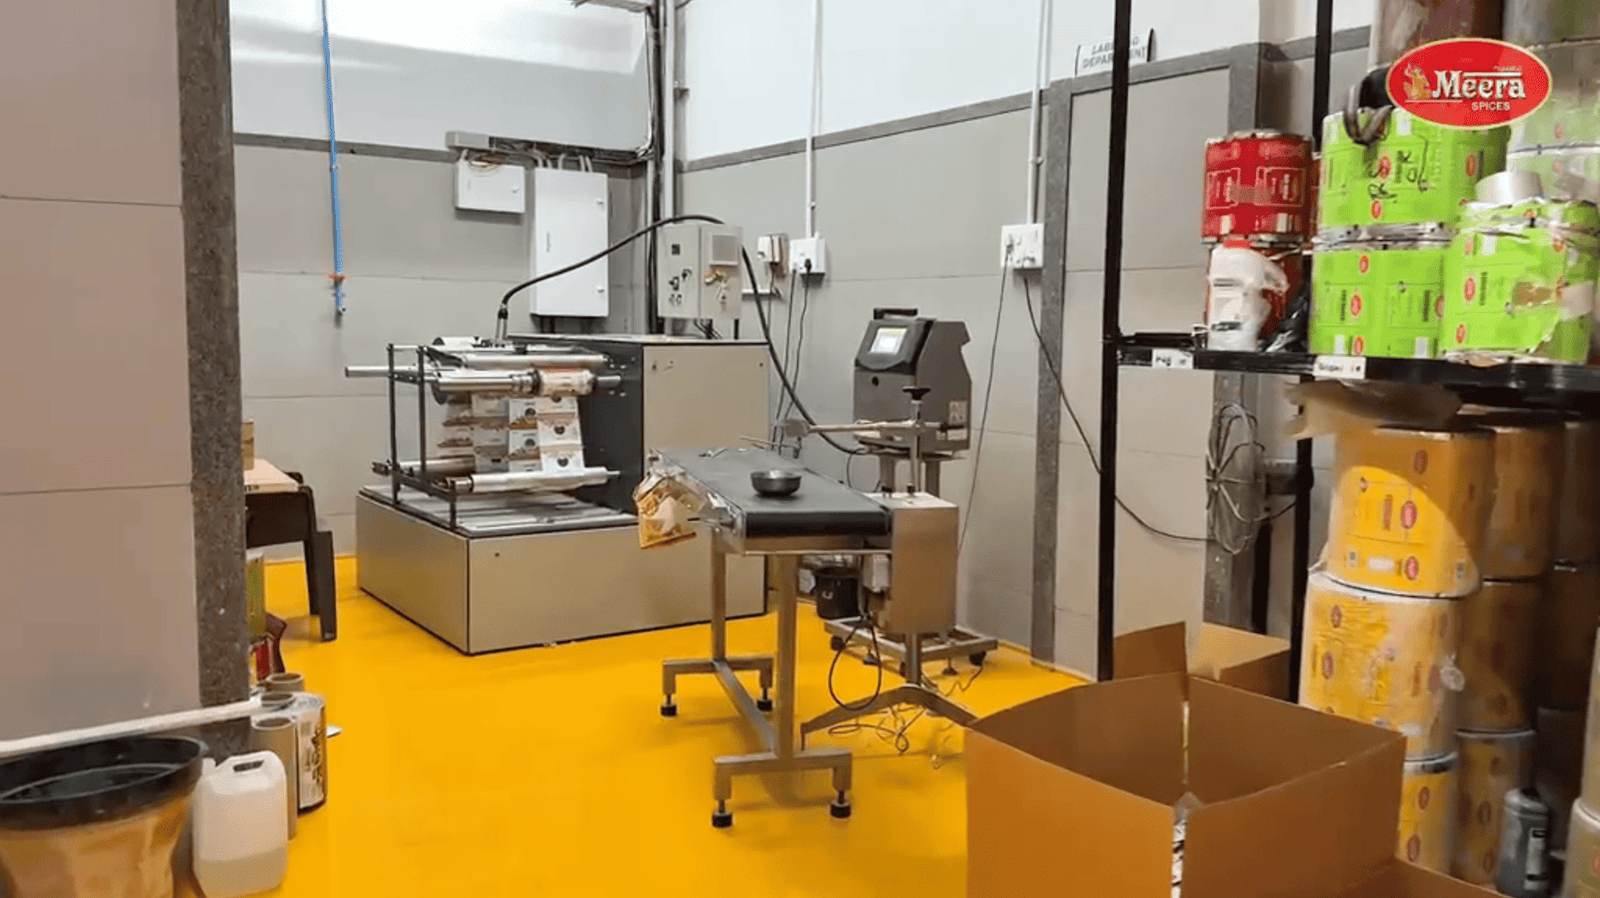
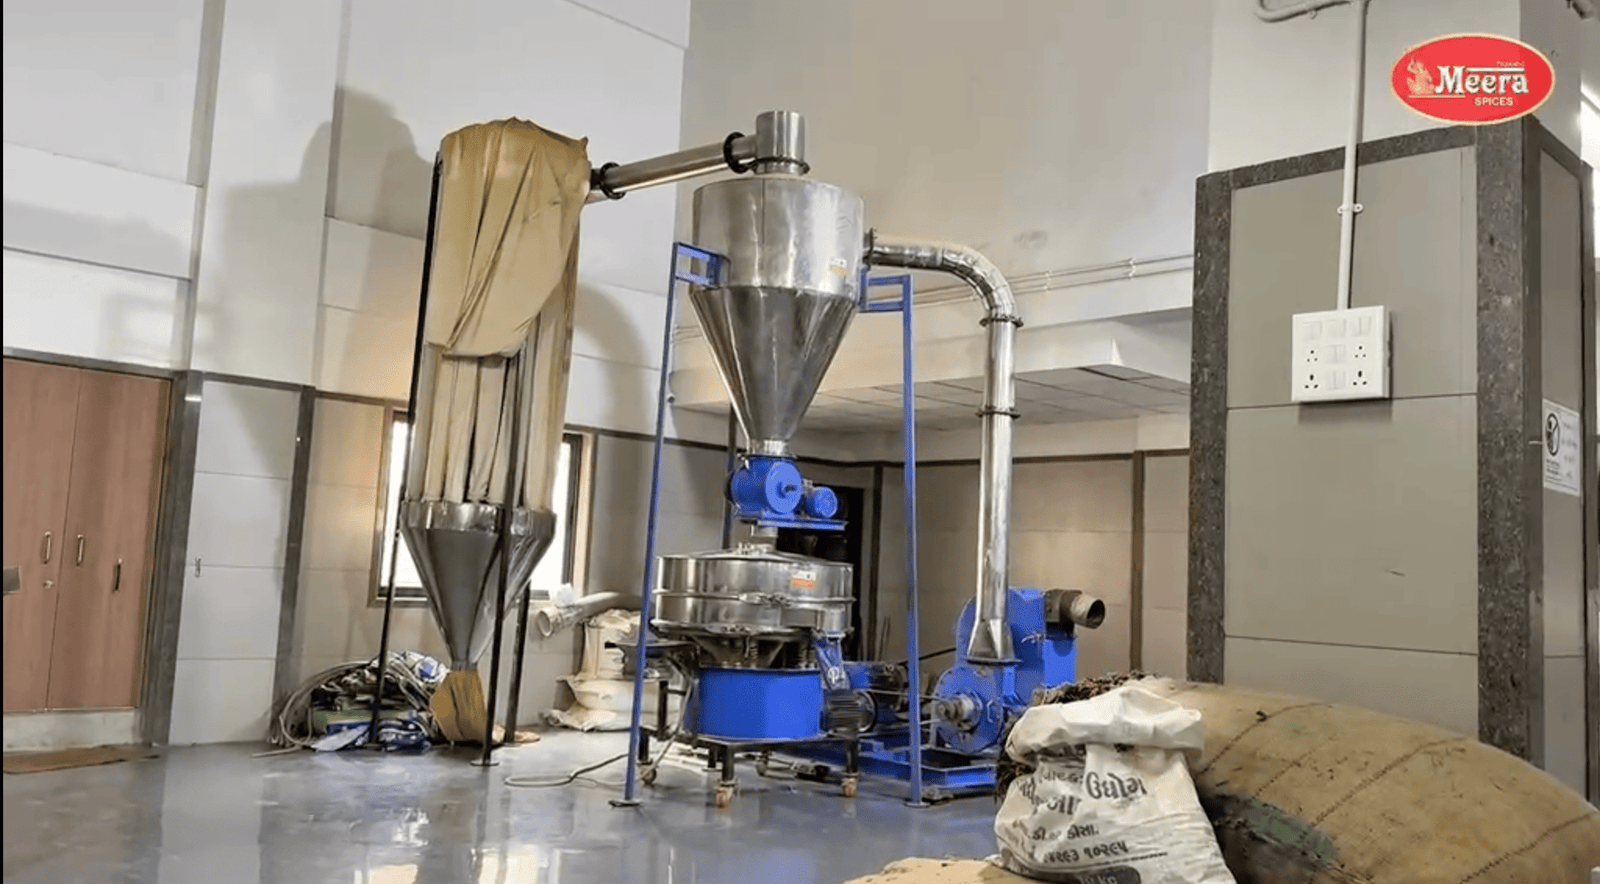
This section shows how our raw spices become high-quality packaged products. Every batch passes through raw material receiving, cleaning, drying (where required), grinding, sieving, blending, quality inspection, packaging, storage, and dispatch with checks at every stage to protect purity, aroma, and safety.
Milestone Successfully Achieved
Our Legacy
Our Vision
To be a globally recognized name in spice manufacturing, delivering consistent quality while supporting responsible and sustainable practices.
Our Mission
To manufacture and supply spices that meet international standards, connecting agricultural origins with kitchens worldwide through reliable processing.
Our food philosophy
Quality control and quality assurance are managed by a dedicated internal team. Checks are carried out across raw materials, processing stages, and finished output. Standard testing and monitoring equipment are used as part of routine operations. Quality practices are embedded within daily manufacturing activities. Records and verification support consistency and compliance. The objective is to maintain reliable output across batches and applications. Food safety and quality responsibility remain central to all operations.
Supplying the Hospitality Industry
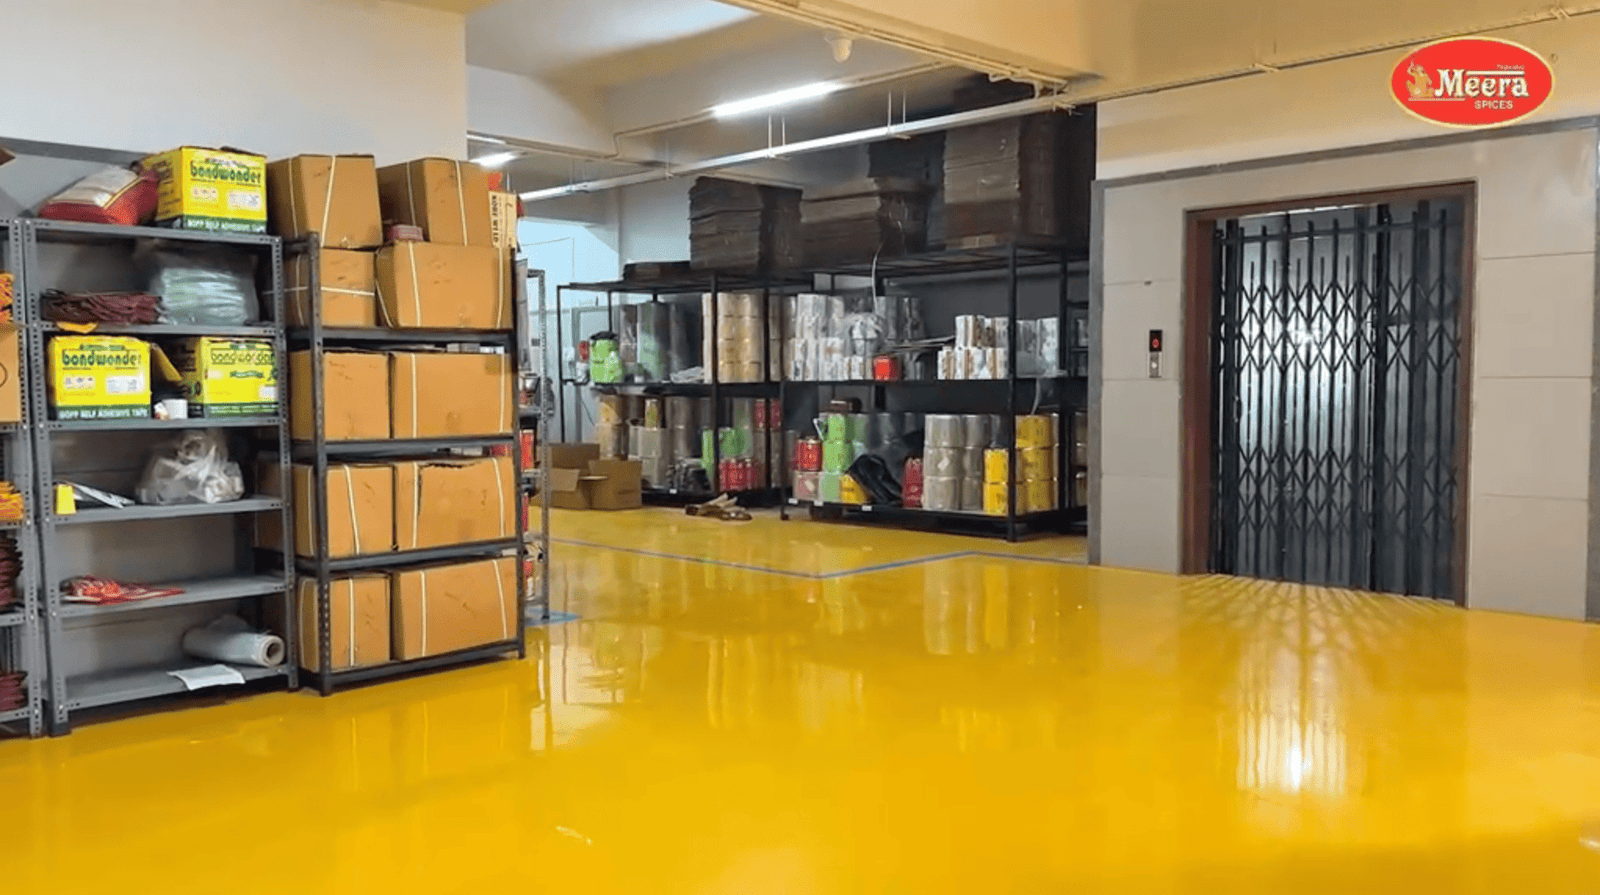
Our advanced manufacturing facility combines modern technology with rigorous quality control to produce spices that meet the highest standards of purity, freshness, and taste.